Choosing the right Chipboard Slotting Machine in 2026 requires more than comparing prices or impressive brochures. Global buyers must examine cutting accuracy, production speed, board compatibility, safety systems, and long-term service support. A machine may look powerful on a showroom floor, yet perform differently with dusty chipboard, uneven sheets, or continuous factory workloads.
This guide reviews leading slotting machines for international purchasing decisions. It focuses on practical performance, including groove depth consistency, feeding stability, blade replacement, dust collection, and control-panel usability. A reliable model should handle common chipboard thicknesses without frequent adjustments. It should also provide clear operating data for production teams. Small details matter. A loose feeder can ruin clean slot alignment within minutes.
The evaluation combines manufacturer information, technical specifications, application experience, and buyer-focused considerations. It also recognizes regional differences in voltage, factory space, maintenance skills, and spare-part availability. No machine is perfect. A lower purchase price may hide expensive downtime, while advanced automation may exceed a small workshop’s needs. That is worth questioning.
The 2026 selection highlights machines suitable for furniture production, cabinet components, packaging structures, and other chipboard applications. Each option deserves careful verification before purchase. Request sample testing. Check service response times. Confirm installation requirements. A dependable supplier should explain limitations honestly, not only advertise maximum output. For global buyers, the best choice is not always the fastest machine. It is the machine that delivers stable results, manageable maintenance, and measurable value over years of operation.
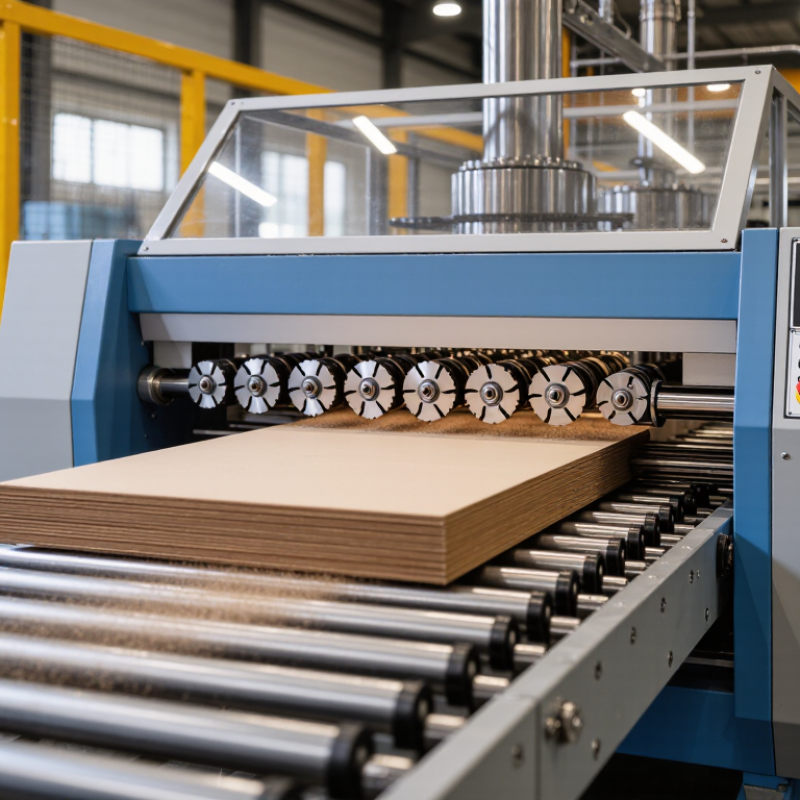
Chipboard slotting machines cut precise grooves, slots, and creases in paperboard sheets. These operations prepare flat blanks for folding cartons, trays, dividers, and protective inserts. Unlike simple die cutters, slotting units remove narrow sections from the board. This creates folding points and locking structures without cutting the entire sheet.
The process starts with sheet feeding and alignment. Rollers guide each sheet beneath rotary knives or adjustable tooling. Scoring wheels compress the board, while slotting knives remove selected strips. Sensors can correct skew, but operators still check the first sheets manually. That practical step matters. A small alignment error can weaken a carton corner.
FAO’s 2022 Forest Products data recorded about 401 million tonnes of global paper and paperboard production. Smithers’ 2024 corrugated packaging outlook also anticipates low-single-digit annual growth through 2029. These figures support continued demand for accurate board-converting equipment, especially in export packaging markets.
However, chipboard is not uniform. Recycled fibers, moisture, coating thickness, and board density change cutting behavior. A machine that performs well on dry, dense stock may struggle with soft recycled sheets.
Buyers should test actual materials, not rely only on rated speed.
Faster is not always better.
Clean slots, stable feeding, and repeatable setup usually matter more than maximum strokes per minute. Reports provide market direction; shop-floor trials reveal the uncomfortable details.
2026 Top Chipboard Slotting Machines for Global Buyers
Chipboard packaging rarely needs one universal slotting machine. Carton blanks, drawer sleeves, and internal dividers demand different cutting behavior. A flatbed slotter suits short runs and varied sizes, especially when prototypes change weekly. Its tooling is easy to adjust, and registration remains visible to the operator. For clean, narrow slots, check blade sharpness, bed flatness, and board moisture. Small shifts can weaken a folding corner.
Rotary slotting machines fit stable, high-volume production. They maintain consistent spacing across thousands of carton blanks and work well with automatic feeding lines. Buyers should compare feeder accuracy, slot depth control, and waste removal. A machine running quickly is not always productive. Excessive dust, crushed edges, or frequent stoppages can erase its apparent speed advantage. Samples should be tested using the actual chipboard grade, not a smoother substitute.
CNC knife slotting machines support custom inserts, display structures, and complex internal partitions. They offer flexible programming without requiring a new die for every design. This flexibility can reduce setup waste, although output may be slower. A useful evaluation includes a one-hour production trial, dimensional checks, and fold testing after slotting. One imperfect assumption deserves attention: wider slots do not always improve assembly. They can create movement inside the package, particularly when recycled board varies in thickness.
When comparing chipboard slotting machines for global production, start with material control, not headline speed. Check the supported board thickness, slot width, and depth range. A reliable machine should maintain clean cuts across single-wall and heavier chipboard sheets. Ask for trial results using your actual board, because recycled fibers can behave unpredictably.
Feed accuracy matters on every carton line. Look for servo-driven positioning, stable rollers, and sensors that detect sheet movement. A small feeding error can misalign several slots. That becomes expensive quickly. Tool changing should be simple, with accessible holders and clear adjustment scales. Operators should not need excessive force or complicated calculations. I have found that quick setup claims sometimes ignore cleaning time and first-piece inspection.
Safety and maintenance deserve equal attention. Confirm guarded cutting areas, emergency stops, electrical compatibility, and documentation for the destination market. Effective dust extraction protects visibility and reduces debris around bearings. Check whether common wear parts are easy to replace locally. Noise levels also matter in a long shift. Ask about measured output at different speeds, not only the maximum figure. Faster is not always better. A stable 2,000 sheets per hour may outperform an inconsistent higher rate. Leave room for doubt, and verify every specification before purchase.
| Machine Configuration | Typical Application | Compatible Board Thickness | Maximum Working Format | Typical Production Speed | Slotting / Creasing Capability | Positioning Accuracy | Changeover Method | Typical Installed Power | Best Fit for Global Buyers |
|---|---|---|---|---|---|---|---|---|---|
| Manual or Semi-Automatic Flatbed Slotter | Short runs, prototypes, sample cartons, rigid box components and custom packaging | 0.8–3.0 mm | Approx. 600 × 900 mm | 8–20 sheets/min | Single-pass slotting and creasing; tool replacement is generally manual | Typically ±0.5–1.0 mm | Manual setup with mechanical stops and gauges | Approx. 2–5 kW | Small converters, packaging studios and low-volume buyers |
| Automatic Flatbed Slotting and Creasing Machine | Folding cartons, drawer boxes, partitions, presentation boxes and regular production work | 0.8–4.0 mm | Approx. 800 × 1,200 mm | 15–40 sheets/min | Programmable slotting, creasing, trimming and repeatable tool positioning | Typically ±0.2–0.5 mm | Digital parameter setting with recipe storage | Approx. 5–12 kW | General-purpose packaging manufacturers requiring flexibility |
| High-Speed Automatic Flatbed Slotter | Medium- to high-volume chipboard cartons, box blanks and standardized packaging formats | 1.0–4.0 mm | Approx. 1,000 × 1,500 mm | 30–70 sheets/min | Multi-tool slotting and creasing with automatic feeding and delivery | Typically ±0.15–0.3 mm | Motorized setup, job memory and quick-change tooling | Approx. 10–25 kW | Factories prioritizing throughput, labor reduction and repeat orders |
| CNC Digital Knife Slotting Table | Prototype development, variable-data packaging, small batches and frequent design changes | 0.5–6.0 mm, depending on knife and material | Approx. 1,000 × 1,600 mm | 5–25 sheets/min | Computer-controlled cutting, slotting, creasing and kiss-cutting without fixed dies | Typically ±0.1–0.3 mm | File-based setup using CAD, DXF, PDF or similar workflows | Approx. 3–10 kW | Buyers handling many SKUs, prototypes and short customized runs |
| Rotary Slotting and Creasing Line | Continuous production of high-volume cartons, trays and repeat-format packaging | 1.0–5.0 mm, depending on board stiffness and tooling | Approx. 1,200 × 2,000 mm | 40–100 sheets/min | Continuous rotary slotting, creasing and optional scoring operations | Typically ±0.3–0.8 mm | Tooling-based setup; fastest when jobs are standardized | Approx. 20–50 kW | Large plants with stable orders and long production runs |
| Inline Feeding and Delivery Slotter | Integrated packaging lines requiring automatic sheet feeding, slotting and stacking | 1.0–4.0 mm | Approx. 800 × 1,300 mm | 25–60 sheets/min | Automatic feeding, slotting, creasing, counting and delivery | Typically ±0.2–0.5 mm | Touchscreen recipes with synchronized feeder and delivery settings | Approx. 12–30 kW | Export-oriented manufacturers seeking consistent labor and output control |
| Heavy-Duty Chipboard Slotter | Thick greyboard, rigid box panels, furniture packaging and reinforced industrial packaging | 2.0–8.0 mm | Approx. 800 × 1,500 mm | 8–30 sheets/min | Deep slotting and controlled creasing with reinforced drive and clamping systems | Typically ±0.3–0.8 mm | Manual or motor-assisted setup, depending on configuration | Approx. 10–30 kW | Users processing dense, laminated or unusually thick chipboard |
In 2026, global buyers should judge chipboard slotting machines by repeatable output, not impressive catalog numbers. A reliable machine must hold slot depth within tight tolerances across long production runs. Ask for test samples using your own board grades. Measure slot width, edge quality, dust levels, and changeover time. A clean cut matters when cartons fold against printed surfaces. So does stable feeding.
Production experience shows that operator access often matters more than maximum speed. Choose controls that display faults clearly and support multiple languages. Confirm voltage, guarding, emergency stops, and electrical documentation for your destination market. Remote diagnostics can reduce delays, but local service capacity remains essential. Request spare-parts lists, response targets, and training records. Check whether technicians understand recycled fiberboard, which can vary in moisture and density. This detail is easy to underestimate.
Buyers should compare total ownership costs, including tooling, energy, maintenance, shipping, and software updates. A low purchase price may hide expensive changeovers or difficult cleaning routines. Inspect the dust collection connection before approving the layout. It may affect worker comfort and product quality. During factory evaluations, record actual cycle times instead of relying on demonstrations. Results can look better than daily production. No selection model is perfect. Leave room for operator feedback after installation. That feedback may challenge the original specification, but it often reveals the machine’s real value.
Selecting a 2026 chipboard slotting machine requires more than checking cutting speed. Installation starts with a level floor, stable anchoring, and enough clearance for sheet loading. Technicians should verify electrical voltage, grounding, compressed-air quality, and emergency-stop access. The ILO estimated 2.93 million work-related deaths globally in 2019, showing why installation discipline cannot be treated as paperwork.
During operation, operators should inspect blades, guards, sensors, and feeding rollers before each shift. Chipboard dust can obscure markings and reduce visibility around the slotting area. Keep hands outside the danger zone, and use approved push tools when adjustment is unavoidable. The U.S. Bureau of Labor Statistics recorded 5,283 fatal occupational injuries in 2023. The figure covers all industries, but it reinforces one point: production pressure must not replace controlled procedures.
Maintenance needs a written schedule based on operating hours, not memory. Clean dust from guides and electrical cabinets, lubricate approved points, and check belt tension weekly. Isolate energy before clearing jams, following ISO 12100 risk-assessment principles and applicable lockout procedures. A checklist helps. It is not perfect. A tired operator may still skip one line, especially during a night shift. Supervisors should record near misses, review training monthly, and replace damaged guards immediately. Safety glasses, hearing protection, and close-fitting clothing remain basic requirements.
Thank you for reaching out.
Your message has been received, and a member of the Bluestem Energy Solutions team will be in touch soon. We appreciate your interest and look forward to connecting.
